This chapter contains the engineering properties and related characteristics of wrought and cast aluminum alloys used in aircraft and missile structural applications.
General comments on engineering properties and the considerations relating to alloy selection are presented in this section. Mechanical and physical property data and characteristics pertinent to specific alloy groups or individual alloys are reported in Sections 3.2 through 3.9. Element properties are presented in Section 3.10.
Aluminum is a lightweight, corrosion-resistant structural material that can be strengthened through alloying and, dependent upon composition, further strengthened by heat treatment and/or cold working [Reference 3.1(a)]. Among its advantages for specific applications are: low density, high strength-to-weight ratio, good corrosion resistance, ease of fabrication and diversity of form.
Wrought and cast aluminum and aluminum alloys are identified by a four-digit numerical designation, the first digit of which indicates the alloy group as shown in Table 3.1. For structural wrought aluminum alloys the last two digits identify the aluminum alloy. The second digit indicates modifications of the original alloy or impurity limits. For cast aluminum and aluminum alloys the second and third digits identify the aluminum alloy or indicate the minimum aluminum percentage. The last digit, which is to the right of the decimal point, indicates the product form: XXX.0 indicates castings, and XXX.1 and XXX.2 indicate ingot.
| Alloy Group | Wrought Alloys — Major Alloying Elements | Alloy Group | Cast Alloys — Major Alloying Groups |
|---|---|---|---|
| 1XXX | 99.00 percent minimum aluminum | 1XX.0 | 99.00 percent minimum aluminum |
| 2XXX | Copper | 2XX.0 | Copper |
| 3XXX | Manganese | 3XX.0 | Silicon with added copper and/or magnesium |
| 4XXX | Silicon | 4XX.0 | Silicon |
| 5XXX | Magnesium | 5XX.0 | Magnesium |
| 6XXX | Magnesium and Silicon | 6XX.0 | Unused Series |
| 7XXX | Zinc | 7XX.0 | Zinc |
| 8XXX | Other Elements | 8XX.0 | Tin |
| 9XXX | Unused Series | 9XX.0 | Other Elements |
The layout of this chapter is in accordance with this four-digit number system for both wrought and cast alloys [Reference 3.1(b)]. Table 3.1.1 is the aluminum alloy index that illustrates both the general section layout as well as details of those specific aluminum alloys presently contained in this chapter. The wrought alloys are in Sections 3.2 through 3.7, whereas the cast alloys are in Sections 3.8 and 3.9.
| Section | Alloy Designation | Section | Alloy Designation |
|---|---|---|---|
| 3.2 | 2000 series wrought alloys | 3.6.2 | 6061 |
| 3.2.1 | 2014 | 3.6.3 | 6151 |
| 3.2.2 | 2017 | 3.7 | 7000 series wrought alloys |
| 3.2.3 | 2024 | 3.7.1 | 7010 |
| 3.2.4 | 2025 | 3.7.2 | 7040 |
| 3.2.5 | 2026 | 3.7.3 | 7049/7149 |
| 3.2.6 | 2090 | 3.7.4 | 7050 |
| 3.2.7 | 2124 | 3.7.5 | 7055 |
| 3.2.8 | 2219 | 3.7.6 | 7075 |
| 3.2.9 | 2297 | 3.7.7 | 7150 |
| 3.2.10 | 2424 | 3.7.8 | 7175 |
| 3.2.11 | 2519 | 3.7.9 | 7249 |
| 3.2.12 | 2524 | 3.7.10 | 7475 |
| 3.2.13 | 2618 | 3.8 | 200.0 series cast alloys |
| 3.3 | 3000 series wrought alloys | 3.8.1 | A201.0 |
| 3.4 | 4000 series wrought alloys | 3.9 | 300.0 series cast alloys |
| 3.5 | 5000 series wrought alloys | 3.9.1 | 354.0 |
| 3.5.1 | 5052 | 3.9.2 | 355.0 |
| 3.5.2 | 5083 | 3.9.3 | C355.0 |
| 3.5.3 | 5086 | 3.9.4 | 356.0 |
| 3.5.4 | 5454 | 3.9.5 | A356.0 |
| 3.5.5 | 5456 | 3.9.6 | A357.0 |
| 3.6 | 6000 series wrought alloys | 3.9.7 | D357.0 |
| 3.6.1 | 6013 | 3.9.8 | 359.0 |
The properties of the aluminum alloys are determined by the alloy content and method of fabrication. Some alloys are strengthened principally by cold work, while others are strengthened principally by solution heat treatment and precipitation hardening [Reference 3.1(a)]. The temper designations, shown in Table 3.1.2 (which is based on Reference 3.1.2), are indicative of the type of strengthening mechanism employed.
Among the properties presented herein, some, such as the room-temperature, tensile, compressive, shear and bearing properties, are either specified minimum properties or derived minimum properties related directly to the specified minimum properties. They may be directly useful in design. Data on the effect of temperature on properties are presented so that percentages may be applied directly to the room-temperature minimum properties. Other properties, such as the stress-strain curve, fatigue and fracture toughness data, and modulus of elasticity values, are presented as average or typical values, which may be used in assessing the usefulness of the material for certain applications. Comments on the effect of temperature on properties are given in Sections 3.1.2.1.7 and 3.1.2.1.8; comments on the corrosion resistance are given in Section 3.1.2.3; and comments on the effects of manufacturing practices on these properties are given in Section 3.1.3.
| Temper | Description |
|---|---|
| Temper Designation Systema,b | |
| The temper designation system is used for all forms of wrought and cast aluminum and aluminum alloys except ingot. It is based on the sequences of basic treatments used to produce the various tempers. The temper designation follows the alloy designation, the two being separated by a hyphen. Basic temper designations consist of letters. Subdivisions of the basic tempers, where required, are indicated by one or more digits following the letter. These designate specific sequences of basic treatments, but only operations recognized as significantly influencing the characteristics of the product are indicated. Should some other variation of the same sequence of basic operations be applied to the same alloy, resulting in different characteristics, then additional digits are added to the designation. | |
| Basic Temper Designations | |
| F | as fabricated. Applies to the products of shaping processes in which no special control over thermal conditions or strain-hardening is employed. For wrought products, there are no mechanical property limits. |
| O | annealed. Applies to wrought products which are annealed to obtain the lowest strength temper, and to cast products which are annealed to improve ductility and dimensional stability. The O may be followed by a digit other than zero. |
| H | strain-hardened (wrought products only). Applies to products which have their strength increased by strain-hardening, with or without supplementary thermal treatments to produce some reduction in strength. The H is always followed by two or more digits. |
| W | solution heat-treated. An unstable temper applicable only to alloys which spontaneously age at room temperature after solution heat-treatment. This designation is specific only when the period of natural aging is indicated: for example, W ½ hr. |
| T | thermally treated to produce stable tempers other than F, O, or H. Applies to products which are thermally treated, with or without supplementary strain-hardening, to produce stable tempers. The T is always followed by one or more digits. |
| Subdivisions of H Temper: Strain-hardened | |
| The first digit following H indicates the specific combination of basic operations, as follows: | |
| H1 | strain-hardened only. Applies to products which are strain-hardened to obtain the desired strength without supplementary thermal treatment. The number following this designation indicates the degree of strain-hardening. |
| H2 | strain-hardened and partially annealed. Applies to products which are strain-hardened more than the desired final amount and then reduced in strength to the desired level by partial annealing. For alloys that age-soften at room temperature, the H2 tempers have the same minimum ultimate tensile strength as the corresponding H3 tempers. For other alloys, the H2 tempers have the same minimum ultimate tensile strength as the corresponding H1 tempers and slightly higher elongation. The number following this designation indicates the degree of strain-hardening remaining after the product has been partially annealed. |
| H3 | strain-hardened and stabilized. Applies to products which are strain-hardened and whose mechanical properties are stabilized either by a low temperature thermal treatment or as a result of heat introduced during fabrication. Stabilization usually improves ductility. This designation is applicable only to those alloys which, unless stabilized, gradually age-soften at room temperature. The number following this designation indicates the degree of strain-hardening remaining after the stabilization treatment. |
| Second digit — degree of strain hardening | |
| The digit following the designations H1, H2, and H3 indicates the degree of strain hardening. Numeral 8 has been assigned to indicate tempers having an ultimate tensile strength equivalent to that achieved by a cold reduction (temperature during reduction not to exceed 120°F) of approximately 75 percent following a full anneal. Tempers between O (annealed) and 8 are designated by numerals 1 through 7. Material having an ultimate tensile strength about midway between that of the O temper and that of the 8 temper is designated by the numeral 4; about midway between the O and 4 tempers by the numeral 2; and about midway between 4 and 8 tempers by the numeral 6. Numeral 9 designates tempers whose minimum ultimate tensile strength exceeds that of the 8 temper by 2.0 ksi or more. For two-digit H tempers whose second digit is odd, the standard limits for ultimate tensile strength are exactly midway between those of the adjacent two digit H tempers whose second digits are even. | |
| NOTE: For alloys which cannot be cold reduced an amount sufficient to establish an ultimate tensile strength applicable to the 8 temper (75 percent cold reduction after full anneal), the 6 temper tensile strength may be established by a cold reduction of approximately 55 percent following a full anneal, and the 4 temper strength may be established by a cold reduction of approximately 35 percent after a full anneal. | |
| Third digit — variation of a two-digit temper | |
| The third digitc, when used, indicates a variation of a two-digit temper. It is used when the degree of control of temper or the mechanical properties or both differ from, but are close to, that (or those) for the two-digit H temper designation to which it is added, or when some other characteristic is significantly affected. | |
| NOTE: The minimum ultimate tensile strength of a three-digit H temper must be at least as close to that of the corresponding two-digit H temper as it is to the adjacent two-digit H tempers. Products of the H temper whose mechanical properties are below H_1 will be variations of H_1. | |
| Three-Digit H Tempers | |
| H_11 | Applies to products which incur sufficient strain hardening after the final anneal that they fail to qualify as annealed but not so much or so consistent an amount of strain hardening that they qualify as H_1. |
| H112 | Applies to products which may acquire some temper from working at an elevated temperature and for which there are mechanical property limits. |
| Subdivisions of T Temper: Thermally Treated | |
| Numerals 1 through 10 following the T indicate specific sequences of basic treatments, as follows.d | |
| T1 | cooled from an elevated temperature shaping process and naturally aged to a substantially stable condition. Applies to products which are not cold worked after cooling from an elevated temperature shaping process, or in which the effect of cold work in flattening or straightening may not be recognized in mechanical property limits. |
| T2 | cooled from an elevated temperature shaping process, cold worked and naturally aged to a substantially stable condition. Applies to products which are cold worked to improve strength after cooling from an elevated temperature shaping process, or in which the effect of cold work in flattening or straightening is recognized in mechanical property limits. |
| T3 | solution heat-treatede, cold worked, and naturally aged to a substantially stable condition. Applies to products which are cold worked to improve strength after solution heat-treatment, or in which the effect of cold work in flattening or straightening is recognized in mechanical property limits. |
| T4 | solution heat-treatede and naturally aged to a substantially stable condition. Applies to products which are not cold worked after solution heat-treatment, or in which the effect of cold work in flattening or straightening may not be recognized in mechanical property limits. |
| T5 | cooled from an elevated temperature shaping process and artificially aged. Applies to products which are not cold worked after cooling from an elevated temperature shaping process, or in which the effect of cold work in flattening or straightening may not be recognized in mechanical property limits. |
| T6 | solution heat-treatede and artificially aged. Applies to products which are not cold worked after solution heat-treatment or in which the effect of cold work in flattening or straightening may not be recognized in mechanical property limits. |
| T7 | solution heat-treatede and overaged/stabilized. Applies to wrought products that are artificially aged after solution heat-treatment to carry them beyond a point of maximum strength to provide control of some significant characteristic. Applies to cast products that are artificially aged after solution heat-treatment to provide dimensional and strength stability. |
| T8 | solution heat-treatede, cold worked, and artificially aged. Applies to products which are cold worked to improve strength, or in which the effect of cold work in flattening or straightening is recognized in mechanical property limits. |
| T9 | solution heat-treatede, artificially aged, and cold worked. Applies to products which are cold worked to improve strength. |
| T10 | cooled from an elevated temperature shaping process, cold worked, and artificially aged. Applies to products which are cold worked to improve strength, or in which the effect of cold work in flattening or straightening is recognized in mechanical property limits. |
| Additional digitsf, the first of which will not be zero, may be added to designations T1 through T10 to indicate a variation in treatment which significantly alters the product characteristicsg that are or would be obtained using the basic treatment. The following specific additional digits have been assigned for stress-relieved tempers of wrought products: | |
| Stress Relieved by Stretching | |
| T_51 | Applies to plate and rolled or cold-finished rod and bar when stretched the indicated amounts after solution heat-treatment or after cooling from an elevated temperature shaping process. The products receive no further straightening after stretching. Plate … 1½ to 3% permanent set. Rolled or Cold-Finished Rod and Bar … 1 to 3% permanent set. Die or Ring Forgings and Rolled Rings … 1 to 5% permanent set. |
| T_510 | Applies to extruded rod, bar, shapes and tube and to drawn tube when stretched the indicated amounts after solution heat-treatment or after cooling from an elevated temperature shaping process. These products receive no further straightening after stretching. Extruded Rod, Bar, Shapes and Tube … 1 to 3% permanent set. Drawn Tube … ½ to 3% permanent set. |
| T_511 | Applies to extruded rod, bar, shapes and tube and to drawn tube when stretched the indicated amounts after solution heat-treatment or after cooling from an elevated temperature shaping process. These products may receive minor straightening after stretching to comply with standard tolerances. |
| Stress Relieved by Compressing | |
| T_52 | Applies to products which are stress-relieved by compressing after solution heat-treatment or cooling from an elevated temperature shaping process to produce a set of 1 to 3 percent. |
| Stress Relieved by Combined Stretching and Compressing | |
| T_54 | Applies to die forgings which are stress relieved by restriking cold in the finish die. |
| NOTE: The same digits (51, 52, 54) may be added to the designation W to indicate unstable solution heat-treated and stress-relieved treatment. | |
| The following temper designations have been assigned for wrought product test material heat-treated from annealed (O, O1, etc.) or F temper.h | |
| T42 | Solution heat-treated from annealed or F temper and naturally aged to a substantially stable condition. |
| T62 | Solution heat-treated from annealed or F temper and artificially aged. |
| Temper designations T42 and T62 may also be applied to wrought products heat-treated from any temper by the user when such heat-treatment results in the mechanical properties applicable to these tempers. | |
| Variations of O Temper: Annealed | |
| A digit following the O, when used, indicates a product in the annealed condition have special characteristics. NOTE: As the O temper is not part of the strain-hardened (H) series, variations of O temper will not apply to products which are strain-hardened after annealing and in which the effect of strain-hardening is recognized in the mechanical properties or other characteristics. | |
| Assigned O Temper Variations | |
| The following temper designation has been assigned for wrought products high temperature annealed to accentuate ultrasonic response and provide dimensional stability. | |
| O1 | Thermally treated at approximately same time and temperature required for solution heat treatment and slow cooled to room temperature. Applicable to products which are to be machined prior to solution heat treatment by the user. Mechanical Property limits are not applicable. |
| Designation of Unregistered Tempers | |
| P | The letter P has been assigned to denote H, T and O temper variations that are negotiated between manufacturer and purchaser. The letter P immediately follows the temper designation that most nearly pertains. Specific examples where such designation may be applied include the following: • The use of the temper is sufficiently limited so as to preclude its registration. (Negotiated H temper variations were formerly indicated by the third digit zero.) • The test conditions (sampling location, number of samples, test specimen configuration, etc.) are different from those required for registration with the Aluminum Association. • The mechanical property limits are not established on the same basis as required for registration with the Aluminum Association. |
| a From reference 3.1.2. | |
| b Temper designations conforming to this standard for wrought aluminum and wrought aluminum alloys, and aluminum alloy castings may be registered with the Aluminum Association provided: (1) the temper is used or is available for use by more than one user, (2) mechanical property limits are registered, (3) characteristics of the temper are significantly different from those of all other tempers which have the same sequence of basic treatments and for which designations already have been assigned for the same alloy and product, and (4) the following are also registered if characteristics other than mechanical properties are considered significant: (a) test methods and limits for the characteristics or (b) the specific practices used to produce the temper. | |
| c Numerals 1 through 9 may be arbitrarily assigned as the third digit and registered with The Aluminum Association for an alloy and product to indicate a variation of a two-digit H temper (see footnote b). | |
| d A period of natural aging at room temperature may occur between or after the operations listed for the T tempers. Control of this period is exercised when it is metallurgically important. | |
| e Solution heat treatment is achieved by heating cast or wrought products to a suitable temperature, holding at that temperature long enough to allow constituents to enter into solid solution and cooling rapidly enough to hold the constituents in solution. Some 6000 series alloys attain the same specified mechanical properties whether furnace solution heat-treated or cooled from an elevated temperature shaping process at a rate rapid enough to hold constituents in solution. In such cases the temper designations T3, T4, T6, T7, T8, and T9 are used to apply to either process and are appropriate designations. | |
| f Additional digits may be arbitrarily assigned and registered with the Aluminum Association for an alloy and product to indicate a variation of tempers T1 through T10 even though the temper representing the basic treatment has not been registered (see footnote b). Variations in treatment which do not alter the characteristics of the product are considered alternate treatments for which additional digits are not assigned. | |
| g For this purpose, characteristics is something other than mechanical properties. The test method and limit used to evaluate material for this characteristic are specified at the time of the temper registration. | |
| h When the user requires capability demonstrations from T-temper, the seller will note “capability compliance” adjacent to the specified ending tempers. Some examples are: “-T4 to -T6 Capability Compliance as for aging” or “-T351 to -T4 Capability Compliance as for resolution heat treating.” | |
It should be recognized not all combinations of stress and environment have been investigated, and it may be necessary to evaluate an alloy under the specific conditions involved for certain critical applications.
3.1.2.1.1 Strength (Tension, Compression, Shear, Bearing) — The design strength properties at room temperature are listed at the beginning of the section covering the properties of an alloy. The effect of temperature on these properties is indicated in figures which follow the tables.
The A- and B-basis values for tensile properties for the direction associated with the specification requirements are based upon a statistical analysis of production quality control data obtained from specimens tested in accordance with procurement specification requirements. For sheet and plate of heat-treatable alloys, the specified minimum values are for the long-transverse (LT) direction, while for sheet and plate of nonheat treatable alloys and for rolled, drawn, or extruded products, the specified minimum values are for the longitudinal (L) direction. For forgings, the specified minimum values are stated for at least two directions. The design tensile properties in other directions and the compression, shear, and bearing properties are “derived” properties, based upon the relationships among the properties developed by tests of at least ten lots of material and applied to the appropriate established A, B, or S properties. All of these properties are representative of the regions from which production quality control specimens are taken, but may not be representative of the entire cross section of products appreciably thicker than the test specimen or products of complex cross sections.
Tensile and compressive strengths are given for the longitudinal, long-transverse, and short-transverse directions wherever data are available. Short-transverse strengths may be relatively low, and transverse properties should not be assumed to apply to the short-transverse direction unless so stated. In those instances where the direction in which the material will be used is not known, the lesser of the applicable longitudinal or transverse properties should be used.
Bearing strengths are given without reference to direction and may be assumed to be about the same in all directions, with the exception of plate, die forging, and hand forging. A reduction factor is used for edgewise bearing load in thick bare and clad plate of 2000 and 7000 series alloys. The results of bearing tests on longitudinal and long-transverse specimens taken edgewise from plate, die forging, and hand forging have shown that the edgewise bearing strengths are substantially lower than those of specimens taken parallel to the surface. The bearing specimen orientations in thick plate are shown in Figure 3.1.2.1.1(a). For plate, bearing specimens are oriented so that the width of the specimen is parallel to the surfaces of the plate (flatwise); consequently, in cases where the stress condition approximates that of the longitudinal or long-transverse edgewise orientations, the reductions in design values shown in Table 3.1.2.1.1 should be made.
It should be noted that in recent years, bearing data have been presented from tests made in accordance with ASTM E 238 which requires clean pins and specimens. See Reference 3.1.2.1.1 for additional information. Designers should consider a reduction factor in applying these values to structural analyses.
For die and hand forgings, bearing specimens are taken edgewise so that no reduction factor is necessary. In the case of die forgings, the location of bearing specimens is shown in Figures 3.1.2.1.1(b) and (c). For die forgings with cross-sectional shapes in the form of an I-beam or a channel, longitudinal bearing specimens are oriented so the width of the specimens is normal to the parting plane (edgewise). The specimens are positioned so the bearing test holes are midway between the parting plane and the top of the flange. The severity of metal flow at the parting plane near the flash can be expected to vary considerably for web-flange type die forgings; therefore, for consistency, the bearing test hole should not be located on the parting plane. However, in the case of large, bulky-type die forgings, with a cross-sectional shape similar to a square, rectangle, or trapezoid, as shown in Figure 3.1.2.1.1(c), longitudinal bearing specimens are oriented edgewise to the parting plane, but the specimens are positioned so the bearing test holes are located on the parting plane. Similarly, for hand forgings, bearing specimens are oriented edgewise and the specimens are positioned at the ½ thickness location.
| Bearing Property Reduction, percent | |
|---|---|
| Thickness (in.) … | 1.001–6.000 |
| Fbru (e/D = 1.5) | 15 |
| Fbru (e/D = 2.0) | 10 |
| Fbry (e/D = 1.5) | 5 |
| Fbry (e/D = 2.0) | 5 |
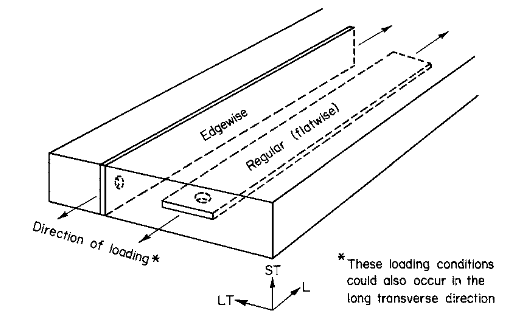
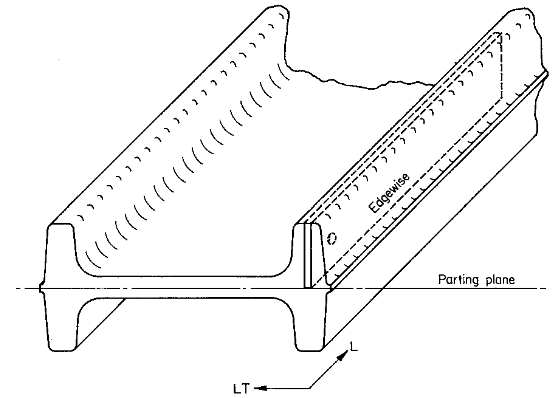
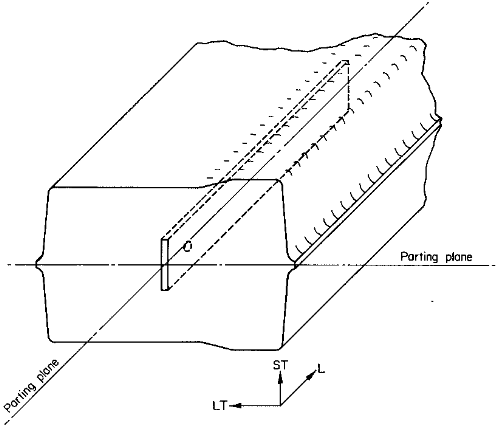
Shear strengths also vary to some extent with plane of shear and direction of loading but the differences are not so consistent [Reference 3.1.2.1.1(c)]. The standard test method for the determination of shear strength of aluminum alloy products, 3/16 inch and greater in thickness, is contained in ASTM B 769.
Shear strength values are presented without reference to grain direction, except for hand forgings. For products other than hand forgings, the lowest shear strength exhibited by tests in the various grain directions is the design value. For hand forgings, the shear strength in short-transverse direction may be significantly lower than for the other two grain directions. Consequently, the shear strength for hand forgings is presented for each grain direction.
For clad sheet and plate (i.e., containing thin surface layers of material of a different composition for added corrosion protection), the strength values are representative of the composite (i.e., the cladding and the core). For sheet and thin plate (≤0.499 inch), the quality-control test specimens are of the full thickness, so that the guaranteed tensile properties and the associated derived values for these products directly represent the composite. For plate ≥0.500 inch in thickness, the quality-control test specimens are machined from the core so the guaranteed tensile properties in specifications reflect the core material only, not the composite. Therefore, the design tensile properties for the thicker material are obtained by adjustment of the specification tensile properties and the other related properties to represent the composite, using the nominal total cladding thickness and the typical tensile properties of the cladding material.
For clad aluminum sheet and plate products, it is also important to distinguish between primary and secondary modulus values. The initial, or primary, modulus represents an average of the elastic moduli of the core and cladding; it applies only up to the proportional limit of the cladding. For example, the primary modulus of 2024-T3 clad sheet applies only up to about 6 ksi. Similarly, the primary modulus of 7075-T6 clad sheet applies only up to approximately 12 ksi. A typical use of primary moduli is for low amplitude, high frequency fatigue.
3.1.2.1.2 Elongation — Elongation values are included in the tables of room-temperature mechanical properties. In some cases where the elongation is a function of material thickness, a supplemental table is provided. Short-transverse elongations may be relatively low, and long-transverse values should not be assumed to apply to the short-transverse direction.
3.1.2.1.3 Stress-Strain Relationship — The stress-strain relationships presented, which include elastic and compressive tangent moduli, are typical curves based on three or more lots of test data. Being typical, these curves will not correspond to yield strength data presented as design allowables (minimum values). However, the stress-strain relationships are no less useful, since there are well-known methods for using these curves in design by reducing them to a minimum curve scaled down from the typical curve or by using Ramberg-Osgood parameters obtained from the typical curves.
3.1.2.1.4 Creep and Stress Rupture — Sustained stressing at elevated temperature sufficient to result in appreciable amounts of creep deformation (e.g., more than 0.2 percent) may result in decreased strength and ductility. It may be necessary to evaluate an alloy under its stress-temperature environment for critical applications where sustained loading is anticipated (see Reference 3.1.2.1.4).
3.1.2.1.5 Fatigue — Fatigue S/N curves are presented for those alloys for which sufficient data are available. Data for both smooth and notched specimens are presented. The data from which the curves were developed were insufficient to establish scatter bands and do not have the statistical reliability of the room-temperature mechanical properties; the values should be considered to be representative for the respective alloys.
The fatigue strengths of aluminum alloys, with both notched and unnotched specimens, are at least as high or higher at subzero temperatures than at room temperature [References 3.1.2.1.5(a) through (c)]. At elevated temperatures, the fatigue strengths are somewhat lower than at room temperature, the difference increasing with increase in temperature.
The data presented do not apply directly to the design of structures because they do not take into account the effect of stress raisers such as reentrant corners, notches, holes, joints, rough surfaces, and other similar conditions which are present in fabricated parts. The localized high stresses induced in fabricated parts by such stress raisers are of much greater importance for repeated loading than they are for static loading and may reduce the fatigue life of fabricated parts far below that which would be predicted by comparing the smooth-specimen fatigue strength directly with the nominal calculated stresses for the parts in question. See References 3.1.2.1.5(d) through (q) for information on how to use high-strength aluminum alloys, Reference 3.1.2.1.5(r) for details on the static and fatigue strengths of high-strength aluminum-alloy bolted joints, Reference 3.1.2.1.5(s) for single-rivet fatigue-test data, and Reference 1.4.9.3(b) for a general discussion of designing for fatigue. Fatigue-crack-growth data are presented in the various alloy sections.
3.1.2.1.6 Fracture Toughness — Typical values of plane-strain fracture toughness, KIc, [Reference 3.1.2.1.6(a)] for the high-strength aluminum alloy products are presented in Table 3.1.2.1.6. Minimum, average, and maximum values as well as coefficient of variation are presented for the alloys and tempers for which valid data are available [References 3.1.2.1.6(b) through (j)]. Although representative, these values do not have the statistical reliability of the room-temperature mechanical properties.
Graphic displays of the residual strength behavior of middle tension panels are presented in the various alloy sections. The points denote the experimental data from which the curve of fracture toughness was derived.
| Alloy/Temperb | Product Form | Orientationc | Product Thickness Range, inches | Number of Sources | Sample Size | Specimen Thickness Range, inches | KIc, ksi√in. | Coefficient of Variation | Minimum Specification Value | ||
|---|---|---|---|---|---|---|---|---|---|---|---|
| Max. | Avg. | Min. | |||||||||
| 2014-T651 | Plate | L-T | ≥0.5 | 1 | 24 | 0.5–1.0 | 25 | 22 | 19 | 8.4 | |
| 2014-T651 | Plate | T-L | ≥0.5 | 2 | 34 | 0.5–1.0 | 23 | 21 | 18 | 6.5 | |
| 2014-T652 | Hand Forging | L-T | ≥0.5 | 2 | 15 | 0.8–2.0 | 48 | 31 | 24 | 21.8 | |
| 2014-T652 | Hand Forging | T-L | ≥0.8 | 2 | 15 | 0.8–2.0 | 30 | 21 | 18 | 14.4 | |
| 2024-T351 | Plate | L-T | ≥1.0 | 2 | 11 | 0.8–2.0 | 43 | 31 | 27 | 16.5 | |
| 2024-T851 | Plate | L-S | 1.4–3.0 | 4 | 11 | 0.5–0.8 | 32 | 25 | 20 | 17.8 | |
| 2024-T851 | Plate | L-T | ≥0.5 | 11 | 102 | 0.4–1.4 | 32 | 23 | 15 | 10.1 | |
| 2024-T851 | Plate | T-L | 0.4–4.0 | 9 | 80 | 0.4–1.4 | 25 | 20 | 18 | 8.8 | |
| 2024-T852 | Forging | T-L | 2.0–7.0 | 3 | 20 | 0.7–2.0 | 25 | 19 | 15 | 15.5 | |
| 2024-T852 | Hand Forging | L-T | ---- | 4 | 35 | 0.8–2.0 | 38 | 28 | 19 | 18.4 | |
| 2024-T852 | Hand Forging | T-L | ---- | 2 | 17 | 0.7–2.0 | 22 | 18 | 14 | 14.4 | |
| 2124-T851 | Plate | L-T | ≥0.8 | 13 | 497 | 0.5–2.5 | 38 | 29 | 18 | 10.4 | 24 |
| 2124-T851 | Plate | T-L | 0.6–6.0 | 10 | 509 | 0.5–2.0 | 32 | 25 | 19 | 9.7 | 20 |
| 2124-T851 | Plate | S-L | ≥0.5 | 6 | 489 | 0.3–1.5 | 27 | 21 | 16 | 9.8 | 18 |
| 2219-T851 | Plate | L-T | ---- | 4 | 67 | 1.0–2.5 | 38 | 33 | 30 | 7.2 | |
| 2219-T851 | Plate | T-L | ≥1.0 | 6 | 108 | 0.8–2.5 | 37 | 29 | 20 | 10.1 | |
| 2219-T851 | Plate | S-L | ≥0.8 | 3 | 24 | 0.5–1.5 | 26 | 22 | 20 | 9.6 | |
| 2219-T851 | Forging | S-L | ---- | 1 | 85 | 1.0–1.5 | 34 | 25 | 19 | 12.1 | |
| 2219-T8511 | Extrusion | T-L | ---- | 1 | 19 | 1.8–2.0 | 34 | 29 | 23 | 12.3 | |
| 2219-T852 | Forging | S-L | ---- | 2 | 60 | 0.8–2.0 | 35 | 25 | 20 | 12.1 | |
| 2219-T852 | Hand Forging | L-T | ---- | 2 | 32 | 1.5–2.5 | 46 | 38 | 30 | 9.7 | |
| 2219-T852 | Hand Forging | T-L | ≥1.5 | 2 | 28 | 1.5–2.5 | 36 | 27 | 22 | 8.4 | |
| 2219-T87 | Plate | L-T | ≥1.5 | 3 | 11 | 0.8–2.0 | 34 | 27 | 25 | 9.3 | |
| 2219-T87 | Plate | T-L | ---- | 1 | 11 | 1.0 | 22 | 22 | 19 | 3.9 | 31 |
| 2297-T87 | Plate | L-T | 3–4 | 1 | 16 | 1.5 | 50 | 40 | 33 | 11.3 | 31 |
| 2297-T87 | Plate | T-L | 3–4 | 1 | 18 | 1.5 | 41 | 32 | 28 | 9.4 | 27 |
| 2297-T87 | Plate | S-L | 3–4 | 1 | 17 | 1.0 | 32 | 25 | 20 | 11.0 | 20 |
| 2297-T87 | Plate | L-T | 4–5 | 1 | 51 | 1.5 | 46 | 38 | 32 | 8.0 | 30 |
| 2297-T87 | Plate | T-L | 4–5 | 1 | 51 | 1.5 | 37 | 30 | 26 | 7.1 | 26 |
| 2297-T87 | Plate | S-L | 4–5 | 1 | 52 | 1.0 | 30 | 24 | 19 | 8.7 | 18 |
| 2297-T87 | Plate | L-T | 5–6 | 1 | 17 | 1.5 | 42 | 36 | 31 | 7.7 | 29 |
| 2297-T87 | Plate | T-L | 5–6 | 1 | 17 | 1.5 | 30 | 27 | 25 | 6.2 | 25 |
| 2297-T87 | Plate | S-L | 5–6 | 1 | 14 | 1.0 | 27 | 23 | 19 | 8.7 | 18 |
| 7040-T7451 | Plate | L-T | 3–4 | 1 | 16 | 2 | 39 | 37 | 34 | 5.2 | 26 |
| 7040-T7451 | Plate | T-L | 3–4 | 1 | 16 | 2 | 31 | 30 | 28 | 2.8 | 24 |
| 7040-T7451 | Plate | S-L | 3–4 | 1 | 14 | 2 | 33 | 31 | 29 | 4.2 | 30 |
| 7040-T7451 | Plate | L-T | 4–5 | 1 | 17 | 2 | 34 | 32 | 31 | 2.0 | 25 |
| 7040-T7451 | Plate | T-L | 4–5 | 1 | 17 | 2 | 27 | 26 | 26 | 1.5 | 24 |
| 7040-T7451 | Plate | S-L | 4–5 | 1 | 17 | 2 | 28 | 26 | 26 | 2.2 | 29 |
| 7040-T7451 | Plate | L-T | 5–6 | 1 | 17 | 2 | 34 | 32 | 30 | 2.7 | 23 |
| 7040-T7451 | Plate | T-L | 5–6 | 1 | 14 | 2 | 28 | 25 | 25 | 3.5 | 24 |
| 7040-T7451 | Plate | S-L | 5–6 | 1 | 16 | 2 | 28 | 27 | 26 | 2.7 | 27 |
| 7040-T7451 | Plate | L-T | 6–7 | 1 | 21 | 2 | 37 | 34 | 30 | 5.9 | 22 |
| 7040-T7451 | Plate | T-L | 6–7 | 1 | 21 | 2 | 29 | 27 | 25 | 2.8 | 23 |
| 7040-T7451 | Plate | S-L | 6–7 | 1 | 21 | 2 | 30 | 29 | 27 | 4.0 | 26 |
| 7040-T7451 | Plate | L-T | 7–8 | 1 | 18 | 2 | 33 | 32 | 30 | 3.2 | 22 |
| 7040-T7451 | Plate | T-L | 7–8 | 1 | 16 | 2 | 29 | 28 | 26 | 2.7 | 23 |
| 7040-T7451 | Plate | S-L | 7–8 | 1 | 13 | 2 | 31 | 29 | 26 | 4.6 | 26 |
| 7040-T7451 | Plate | L-T | 8–8.5 | 1 | 17 | 2 | 34 | 31 | 28 | 4.6 | 22 |
| 7040-T7451 | Plate | T-L | 8–8.5 | 1 | 13 | 2 | 26 | 24 | 23 | 5.0 | 22 |
| 7040-T7451 | Plate | S-L | 8–8.5 | 1 | 17 | 2 | 27 | 26 | 25 | 2.1 | |
| 7049-T73 | Die Forging | L-T | 1.4 | 3 | 21 | 0.5–1.0 | 34 | 30 | 27 | 7.4 | |
| 7049-T73 | Die Forging | S-L | ≥0.5 | 3 | 46 | 0.5–1.0 | 26 | 22 | 18 | 9.7 | |
| 7049-T73 | Hand Forging | L-T | ≥0.5 | 2 | 28 | 0.5–1.0 | 37 | 30 | 23 | 12.1 | |
| 7049-T73 | Hand Forging | T-L | 2.0–7.1 | 2 | 27 | 1.0 | 28 | 22 | 18 | 12.5 | |
| 7049-T73 | Hand Forging | S-L | 1.0 | 2 | 24 | 0.8–1.0 | 22 | 19 | 14 | 14.2 | |
| 7050-T7351 | Plate | L-T | 1.0–6.0 | 2 | 31 | 1.0–2.0 | 43 | 35 | 28 | 11.3 | |
| 7050-T7351 | Plate | T-L | 2.0–6.0 | 1 | 29 | 1.5–2.0 | 35 | 30 | 25 | 8.5 | |
| 7050-T7351 | Plate | S-L | 2.0–6.0 | 1 | 30 | 0.8–1.5 | 30 | 28 | 25 | 4.6 | |
| 7050-T74 | Die Forging | S-L | 0.6–7.1 | 3 | 12 | 0.6–2.0 | 27 | 24 | 21 | 8.8 | d |
| 7050-T7451 | Plate | L-T | ---- | 13 | 96 | 1.0–2.0 | 39 | 32 | 25 | 11.7 | d |
| 7050-T7451 | Plate | T-L | ≥1.0 | 9 | 97 | 0.5–2.0 | 38 | 28 | 21 | 15.6 | d |
| 7050-T7451 | Plate | S-L | ≥1.0 | 6 | 44 | 0.7–2.0 | 28 | 23 | 21 | 6.3 | d |
| 7050-T7452 | Hand Forging | L-T | 3.5–5.5 | 1 | 11 | 1.5 | 34 | 31 | 26 | 8.0 | d |
| 7050-T7452 | Hand Forging | T-L | 3.5–7.5 | 1 | 13 | 1.5 | 22 | 21 | 18 | 6.7 | |
| 7050-T7452 | Hand Forging | S-L | 3.5–7.5 | 1 | 17 | 0.8–1.5 | 21 | 19 | 16 | 7.5 | |
| 7050-T76511 | Extrusion | L-T | ---- | 2 | 38 | 0.6–2.0 | 40 | 31 | 27 | 7.8 | |
| 7075-T651 | Plate | L-T | ≥0.6 | 7 | 99 | 0.5–2.0 | 30 | 26 | 20 | 7.6 | |
| 7075-T651 | Plate | T-L | ≥0.5 | 5 | 135 | 0.4–2.0 | 27 | 22 | 18 | 8.9 | |
| 7075-T651 | Plate | S-L | ---- | 2 | 37 | 0.5–1.5 | 22 | 18 | 14 | 10.4 | |
| 7075-T6510 | Extrusion | L-T | 0.7–3.5 | 1 | 26 | 0.5–1.2 | 32 | 27 | 23 | 7.8 | |
| 7075-T6510 | Extrusion | T-L | 0.7–3.5 | 1 | 25 | 0.5–1.2 | 28 | 24 | 21 | 8.0 | |
| 7075-T6510 | Forged Bar | L-T | 0.7–5.0 | 1 | 13 | 0.6–2.0 | 35 | 29 | 24 | 11.6 | |
| 7075-T6510 | Forged Bar | T-L | 0.7–5.0 | 1 | 13 | 0.5–2.5 | 24 | 21 | 17 | 8.2 | |
| 7075-T73 | Die Forging | T-L | ≥0.5 | 1 | 22 | 0.5–0.8 | 25 | 21 | 18 | 9.9 | |
| 7075-T73 | Hand Forging | L-T | ---- | 2 | 10 | 1.0–1.5 | 39 | 31 | 29 | 8.8 | |
| 7075-T73 | Hand Forging | T-L | ≥1.0 | 2 | 14 | 1.0–1.5 | 27 | 23 | 20 | 9.0 | |
| 7075-T7351 | Plate | L-T | ≥1.0 | 8 | 65 | 0.5–2.0 | 36 | 30 | 25 | 8.2 | |
| 7075-T7351 | Plate | T-L | ≥0.5 | 6 | 56 | 0.5–2.0 | 47 | 27 | 21 | 20.1 | |
| 7075-T7351 | Plate | S-L | ≥0.5 | 3 | 20 | 0.5–1.5 | 38 | 22 | 17 | 32.5 | |
| 7075-T73511 | Extrusion | T-L | 1.0–7.0 | 1 | 19 | 0.9–1.0 | 22 | 20 | 19 | 3.7 | |
| 7075-T73511 | Extrusion | L-T | ≥0.9 | 3 | 28 | 0.7–2.0 | 43 | 35 | 31 | 9.4 | |
| 7075-T73511 | Extrusion | T-L | ≥0.7 | 3 | 35 | 0.5–1.8 | 35 | 23 | 12 | 20.3 | |
| 7075-T73511 | Extrusion | S-L | ≥0.5 | 3 | 15 | 0.4–1.0 | 22 | 20 | 17 | 9.0 | |
| 7075-T7352 | Hand Forging | L-T | ---- | 2 | 27 | 0.8–2.0 | 39 | 33 | 30 | 9.2 | |
| 7075-T7352 | Hand Forging | T-L | ≥0.8 | 3 | 20 | 0.8–2.0 | 33 | 26 | 23 | 9.9 | |
| 7075-T7651 | Plate | L-T | ≥0.8 | 6 | 82 | 0.5–2.0 | 43 | 29 | 22 | 17.8 | |
| 7075-T7651 | Plate | T-L | ≥0.5 | 7 | 96 | 0.5–2.0 | 28 | 23 | 20 | 7.6 | |
| 7075-T7651 | Plate | S-L | ≥0.5 | 5 | 28 | 0.4–0.8 | 20 | 18 | 15 | 7.7 | |
| 7075-T7651 | Clad Plate | L-T | 0.5–0.6 | 2 | 30 | 0.5–0.6 | 30 | 25 | 22 | 7.1 | |
| 7075-T7651 | Clad Plate | T-L | 0.5–0.6 | 2 | 56 | 0.5–0.6 | 28 | 24 | 21 | 7.7 | |
| 7075-T76511 | Extrusion | L-T | 1.3–7.0 | 4 | 11 | 1.2–2.0 | 41 | 35 | 31 | 11.0 | |
| 7075-T76511 | Extrusion | T-L | 1.2 | 3 | 42 | 0.6–2.0 | 36 | 23 | 20 | 15.5 | |
| 7150-T77511 | Extrusion | L-T | 0.76 | 1 | 52 | 0.5 | 36 | 31 | 26 | 7.7 | 24 |
| 7150-T77511 | Extrusion | T-L | 0.76 | 1 | 52 | 0.5 | 27 | 24 | 21 | 5.1 | 20 |
| 7175-T6/T6511 | Extrusion | T-L | ---- | 2 | 25 | 0.8–1.0 | 24 | 21 | 18 | 7.9 | |
| 7175-T651 | Plate | L-T | ---- | 1 | 17 | 0.7–0.8 | 30 | 26 | 24 | 9.2 | |
| 7175-T651 | Plate | T-L | ---- | 1 | 10 | 0.7–0.8 | 26 | 22 | 20 | 9.8 | |
| 7175-T6511 | Extrusion | L-T | ---- | 2 | 14 | 0.8–1.0 | 36 | 32 | 24 | 13.8 | |
| 7175-T7351 | Plate | L-T | ---- | 2 | 30 | 0.7–1.6 | 36 | 33 | 32 | 3.3 | |
| 7175-T7351 | Plate | T-L | ---- | 2 | 32 | 0.7–1.6 | 30 | 27 | 25 | 4.5 | |
| 7175-T73511 | Extrusion | L-T | ≥0.7 | 5 | 43 | 0.5–1.5 | 47 | 33 | 23 | 16.0 | 30 |
| 7175-T73511 | Extrusion | T-L | ≥0.5 | 5 | 43 | 0.5–1.0 | 35 | 25 | 20 | 10.9 | 22 |
| 7175-T74 | Die Forging | L-T | ≥0.5 | 3 | 14 | 0.5–1.0 | 38 | 30 | 22 | 15.0 | 27 |
| 7175-T74 | Die Forging | T-L | ≥0.5 | 2 | 13 | 0.5–1.0 | 33 | 24 | 21 | 15.7 | 21 |
| 7175-T74 | Die Forging | S-L | ≥0.5 | 4 | 41 | 0.5–0.8 | 31 | 26 | 20 | 8.6 | 21 |
| 7175-T74 | Hand Forging | T-L | 3.0–5.0 | 2 | 10 | 1.0–1.5 | 29 | 26 | 24 | 4.8 | 25 |
| 7175-T7651 | Clad Plate | L-T | ---- | 1 | 53 | 1.5 | 33 | 32 | 30 | 4.3 | |
| 7175-T7651 | Clad Plate | T-L | ---- | 1 | 50 | 0.6 | 28 | 27 | 25 | 3.1 | |
| 7175-T7651 | Plate | L-T | ---- | 1 | 12 | 1.5 | 32 | 32 | 31 | 1.7 | |
| 7175-T7651 | Plate | T-L | ---- | 1 | 11 | 1.5 | 26 | 25 | 24 | 3.3 | |
| 7175-T76511 | Extrusion | L-T | 1.4–3.8 | 2 | 48 | 0.6–2.0 | 39 | 33 | 27 | 10.7 | |
| 7175-T76511 | Extrusion | T-L | ≥0.6 | 4 | 49 | 0.6–1.8 | 31 | 22 | 20 | 9.8 | |
| 7475-T651 | Plate | L-T | ---- | 3 | 34 | 0.9–2.0 | 49 | 38 | 33 | 9.2 | 30 |
| 7475-T651 | Plate | T-L | 0.6–2.0 | 2 | 143 | 0.6–2.0 | 43 | 34 | 27 | 9.8 | 28 |
| 7475-T651 | Plate | S-L | ≥0.6 | 1 | 23 | 0.5–1.0 | 36 | 28 | 20 | 14.9 | |
| 7475-T7351 | Plate | L-T | 1.3–4.0 | 8 | 151 | 1.3–3.0 | 60 | 47 | 34 | 10.4 | d |
| 7475-T7351 | Plate | T-L | ≥1.3 | 7 | 132 | 0.7–3.0 | 50 | 37 | 29 | 10.4 | d |
| 7475-T7351 | Plate | S-L | ≥0.7 | 7 | 74 | 0.5–1.5 | 36 | 30 | 25 | 8.7 | 25 |
| 7475-T7651 | Plate | L-T | 1.0–2.0 | 4 | 10 | 1.0–2.0 | 46 | 41 | 36 | 6.2 | 33 |
| 7475-T7651 | Plate | T-L | ≥1.0 | 2 | 15 | 0.9–2.0 | 50 | 36 | 29 | 14.5 | 30 |
| a These values are for information only. | |||||||||||
| b Products that do not receive a mechanical stress-relieving process (e.g. -T73 & -T74 tempers) have the potential for induced residual stresses. As a result, care must be taken to prevent fracture toughness properties from bias resulting from residual stresses. | |||||||||||
| c Refer to Figure 1.4.12.3 for definition of symbols. | |||||||||||
| d Varies with thickness. | |||||||||||
3.1.2.1.7 Cryogenic Temperatures — In general, the strengths (including fatigue strengths) of aluminum alloys increase with decrease in temperature below room temperature [References 3.1.2.1.7(a) and (b)]. The increase is greatest over the range from about −100 to −423°F (liquid hydrogen temperature); the strengths at −452°F (liquid helium temperature) are nearly the same as at −423°F [References 3.1.2.1.7(c) and (d)]. For most alloys, elongation and various indices of toughness remain nearly constant or increase with decrease in temperature, while for the 7000 series, modest reductions are observed [References 3.1.2.1.7(d) and (e)]. None of the alloys exhibit a marked transition in fracture resistance over a narrow range of temperature indicative of embrittlement.
The tensile and shear moduli of aluminum alloys also increase with decreasing temperature so that at −100, −320, and −423°F, they are approximately 5, 12, and 16 percent, respectively, above the room temperature values [Reference 3.1.2.1.7(f)].
3.1.2.1.8 Elevated Temperatures — In general, the strengths of aluminum alloys decrease and toughness increases with increase in temperature and with time at temperature above room temperature; the effect is generally greatest over the temperature range from 212 to 400°F. Exceptions to the general trends are tempers developed by solution heat treatment without subsequent aging, for which the initial elevated temperature exposure results in some age hardening and reduction in toughness; further time at temperature beyond that required to achieve peak hardness results in the aforementioned decrease in strength and increase in toughness [Reference 3.1.2.1.8].
Where available from the literature, the average values of certain physical properties are included in the room-temperature tables for each alloy. These properties include density, ρ, in lb/in.3; the specific heat, C, in Btu/(lb)(°F); the thermal conductivity, K, in Btu/[(hr)(ft2)(°F)/ft]; and the mean coefficient of thermal expansion, α, in in./in./°F. Where more extensive data are available to show the effect of temperature on these physical properties, graphs of physical property as a function of temperature are presented for the applicable alloys.
3.1.2.3.1 Resistance to Stress-Corrosion Cracking [see References 3.1.2.3.1(a) through (d)] — In-service stress-corrosion cracking failures can be caused by stresses produced from a wide variety of sources, including solution heat treatment, straightening, forming, fit-up, clamping, and sustained service loads. These stresses may be tensile or compressive, and the stresses due to Poisson effects should not be ignored because SCC failures can be caused by sustained shear stresses. Pin-hole flaws in some corrosion protection coatings may also be sufficient to allow SCC to occur. The high-strength heat treatable wrought aluminum alloys in certain tempers are susceptible to stress-corrosion cracking, depending upon product, section size, direction and magnitude of stress. These alloys include 2014, 2025, 2618, 7075, 7150, 7175, and 7475 in the T6-type tempers and 2014, 2024, 2124, and 2219 in the T3 and T4-type tempers. Other alloy-temper combinations, notably 2024, 2124, 2219, and 2519 in the T6- or T8-type tempers and 7010, 7049, 7050, 7075, 7149, 7175, and 7475 in the T73-type tempers, are decidedly more resistant and sustained tensile stresses of 50 to 75 percent of the minimum yield strength may be permitted without concern about stress corrosion cracking. The T74 and T76 tempers of 7010, 7075, 7475, 7049, 7149, and 7050 provide an intermediate degree of resistance to stress-corrosion cracking, i.e., superior to that of the T6 temper, but not as good as that of the T73 temper of 7075. To assist in the selection of materials, letter ratings indicating the relative resistance to stress-corrosion cracking of various mill product forms of the wrought 2000, 6000, and 7000 series heat-treated aluminum alloys are presented in Table 3.1.2.3.1(a). This table is based upon ASTM G 64 which contains more detailed information regarding this rating system and the procedure for determining the ratings. In addition, more quantitative information in the form of the maximum specified tension stresses at which test specimens will not fail when subjected to the alternate immersion stress-corrosion test described in ASTM G 47 are shown in Tables 3.1.2.3.1(b) through (e) for various heat-treated aluminum product forms, alloys, and tempers.
Where short times at elevated temperatures of 150 to 500°F may be encountered, the precipitation heat-treated tempers of 2024 and 2219 alloys are recommended over the naturally aged tempers.
Alloys 5083, 5086, and 5456 should not be used under high constant applied stress for continuous service at temperatures exceeding 150°F, because of the hazard of developing susceptibility to stress-corrosion cracking. In general, the H34 through H38 tempers of 5086, and the H32 through H38 tempers of 5083 and 5456 are not recommended, because these tempers can become susceptible to stress-corrosion cracking.
For the cold forming of 5083 sheet and plate in the H112, H321, H323, and H343 tempers and 5456 sheet and plate in the H112 and H321 tempers, a minimum bend radius of 5T should be used. Hot forming of the O temper for alloys 5083 and 5456 is recommended, and is preferred to the cold worked tempers to avoid excessive cold work and high residual stress. If the cold worked tempers are heat-treatable alloys are heated for hot forming, a slight decrease in mechanical properties, particularly yield strength, may result.
| Alloy and Temperb | Test Directionc | Rolled Plate | Rod and Bard | Extruded Shapes | Forging |
|---|---|---|---|---|---|
| 2014-T6 | L | A | A | A | B |
| LT | Be | D | Be | Be | |
| ST | D | D | D | D | |
| 2024-T3, T4 | L | A | A | A | f |
| LT | Be | D | Be | f | |
| ST | D | D | D | f | |
| 2024-T6 | L | f | A | f | A |
| LT | f | B | f | Ae | |
| ST | f | B | f | D | |
| 2024-T8 | L | A | A | A | A |
| LT | A | A | A | A | |
| ST | B | A | B | C | |
| 2124-T8 | L | A | f | f | f |
| LT | A | f | f | f | |
| ST | B | f | f | f | |
| 2219-T351X, T37 | L | A | f | A | f |
| LT | B | f | B | f | |
| ST | D | f | D | f | |
| 2219-T6 | L | A | A | A | A |
| LT | A | A | A | A | |
| ST | A | A | A | A | |
| 2219-T85XX, T87 | L | A | f | A | A |
| LT | A | f | A | A | |
| ST | A | f | A | A | |
| 6061-T6 | L | A | A | A | A |
| LT | A | A | A | A | |
| ST | A | A | A | A | |
| 7040-T7451 | L | A | f | f | f |
| LT | A | f | f | f | |
| ST | B | f | f | f | |
| 7049-T73 | L | A | f | A | A |
| LT | A | f | A | A | |
| ST | A | f | B | A | |
| 7049-T76 | L | f | f | A | f |
| LT | f | f | A | f | |
| ST | f | f | C | f | |
| 7050-T74 | L | A | f | A | A |
| LT | A | f | A | A | |
| ST | B | f | B | B | |
| 7050-T76 | L | A | A | A | f |
| LT | A | B | A | f | |
| ST | C | B | C | f | |
| 7075-T6 | L | A | A | A | A |
| LT | Be | D | Be | Be | |
| ST | D | D | D | D | |
| 7075-T73 | L | A | A | A | A |
| LT | A | A | A | A | |
| ST | A | A | A | A | |
| 7075-T74 | L | f | f | f | A |
| LT | f | f | f | A | |
| ST | f | f | f | B | |
| 7075-T76 | L | A | f | A | f |
| LT | A | f | A | f | |
| ST | C | f | C | f | |
| 7149-T73 | L | f | f | A | A |
| LT | f | f | A | A | |
| ST | f | f | B | A | |
| 7175-T74 | L | f | f | f | A |
| LT | f | f | f | A | |
| ST | f | f | f | B | |
| 7475-T6 | L | A | f | f | f |
| LT | Be | f | f | f | |
| ST | D | f | f | f | |
| 7475-T73 | L | A | f | f | f |
| LT | A | f | f | f | |
| ST | A | f | f | f | |
| 7475-T76 | L | A | f | f | f |
| LT | A | f | f | f | |
| ST | C | f | f | f | |
| a Ratings were determined from stress corrosion tests performed on at least ten random lots for which test results showed 90% conformance with 95% confidence when tested at the following stresses. | |||||
| A — Equal to or greater than 75% of the specified minimum yield strength. A very high rating. SCC not anticipated in general applications if the total sustained tensile stress* is less than 75% of the specified minimum yield stress for the alloy, heat treatment, product form, and orientation. | |||||
| B — Equal to or greater than 50% of the specified minimum yield strength. A high rating. SCC not anticipated if the total sustained tensile stress* is less than 50% of the specified minimum yield stress. | |||||
| C — Equal to or greater than 25% of the specified minimum yield stress or 14.5 ksi, whichever is higher. An intermediate rating. SCC not anticipated if the total sustained tensile stress* is less than 25% of the specified minimum yield stress. This rating is designated for the short transverse direction in improved products used primarily for high resistance to exfoliation corrosion in relatively thin structures where applicable short transverse stresses are unlikely. | |||||
| D — Fails to meet the criterion for the rating C. A low rating. SCC failures have occurred in service or would be anticipated if there is any sustained tensile stress* in the designated test direction. This rating currently is designated only for the short transverse direction in certain materials. | |||||
| NOTE — The above stress levels are not to be interpreted as “threshold” stresses, and are not recommended for design. Other documents, such as MIL-STD-1568, NAS SD-24, and MSFC-SPEC-522A, should be consulted for design recommendations. | |||||
| b The ratings apply to standard mill products in the types of tempers indicated, including stress-relieved tempers, and could be invalidated in some cases by application of nonstandard thermal treatments of mechanical deformation at room temperature by the user. | |||||
| c Test direction refers to orientation of the stressing direction relative to the directional grain structure typical of wrought materials, which in the case of extrusions and forgings may not be predictable from the geometrical cross section of the product. L—Longitudinal: parallel to the direction of principal metal extension during manufacture of the product. LT—Long Transverse: perpendicular to direction of principal metal extension. In products whose grain structure clearly shows directionality (width to thickness ratio greater than two) it is that perpendicular direction parallel to the major grain dimension. ST—Short Transverse: perpendicular to direction of principal metal extension and parallel to minor dimension of grains in products with significant grain directionality. | |||||
| d Sections with width-to-thickness ratio equal to or less than two for which there is no distinction between LT and ST. | |||||
| e Rating is one class lower for thicker sections: extrusion, 1 inch and over; plate and forgings, 1.5 inches and over. | |||||
| f Ratings not established because the product is not offered commercially. | |||||
| * The sum of all stresses, including those from service loads (applied), heat treatment, straightening, forming, etc. | |||||
| NOTE: This table is based upon ASTM G 64. | |||||
| Transcription note: Ratings are reproduced exactly as published in MIL-HDBK-5; no values have been altered or corrected. | |||||
| Alloy and Temper | Test Direction | Thickness, inches | Stress, ksi | Referenced Specifications |
|---|---|---|---|---|
| 2024-T851 | ST | 1.001–4.000 | 28b | Company specification |
| 4.001–6.000 | 27b | |||
| 2090-T81c | ST | 0.750–1.500 | 20 | AMS 4303 |
| 2124-T851 | ST | 1.500–1.999 | 28b | AMS 4101 |
| 2.000–4.000 | 28b | AMS-QQ-A-0025/29, ASTM B 209, AMS 4101 | ||
| 4.001–6.000 | 27b | |||
| 2124-T8151c | ST | 1.500–3.000 | 30b | AMS 4221 |
| 3.001–5.000 | 29b | |||
| 5.001–6.000 | 28b | |||
| 2219-T851 | ST | 0.750–2.000 | 34d | AMS-QQ-A-250/30 |
| 2.001–4.000 | 33d | |||
| 4.001–5.000 | 32d | |||
| 5.001–6.000 | 31d | |||
| 2219-T87 | ST | 0.750–3.000 | 38d | AMS-QQ-A-250/30 |
| 3.001–4.000 | 37d | |||
| 4.001–5.000 | 36d | |||
| 2519-T87 | ST | 0.750–4.000 | 43d | MIL-A-46192 |
| 7010-T7351c | ST | 0.750–3.000 | 41d | AMS 4203 |
| 3.001–5.000 | 40d | |||
| 5.001–5.500 | 39d | |||
| 7010-T7451 | ST | 0.750–3.000 | 31b | AMS 4205 |
| 3.001–5.500 | 35 | |||
| 7010-T7651 | ST | 0.750–5.500 | 25 | AMS 4204 |
| 7049-T7351 | ST | 0.750–5.000 | 45 | AMS 4200 |
| 7050-T7451 | ST | 0.750–6.000 | 35 | AMS 4050 |
| 7050-T7651 | ST | 0.750–3.000 | 25 | AMS 4201 |
| 7075-T7351 | ST | 0.750–2.000 | 42d | AMS-QQ-A-250/12, AMS 4078, ASTM B 209 |
| 2.001–2.500 | 39d | |||
| 2.501–4.000 | 36d | |||
| 7075-T7651 | ST | 0.750–1.000 | 25 | AMS-QQ-A-00250/24, ASTM B 209 |
| Clad 7075-T7651 | ST | 0.750–1.000 | 25 | AMS-QQ-A-00250/25, ASTM B 209 |
| 7150-T7751 | ST | 0.750–3.000 | 25 | AMS 4252 |
| 7475-T7351 | ST | 0.750–4.000 | 40 | AMS 4202 |
| 7475-T7651 | ST | 0.750–1.500 | 25 | AMS 4089 |
| a Most specifications reference ASTM G 47, which requires exposures of 10 days for 2XXX alloys and 20 days for 7XXX alloys in ST test direction. | ||||
| b 50% of specified minimum long transverse yield strength. | ||||
| c Design values are not included in MIL-HDBK-5. | ||||
| d 75% of specified minimum long transverse yield strength. | ||||
| DO NOT USE STRESS VALUES FOR DESIGN | ||||
| Alloy and Temper | Product Form | Test Direction | Thickness, inches | Stress, ksi | Referenced Specifications |
|---|---|---|---|---|---|
| 7075-T73-T7351 | Rolled Bar and Rod | ST | 0.750–3.000 | 42b | AMS-QQ-A-225/9, AMS 4124, ASTM B211 |
| 2219-T8511 | Extrusion | ST | 0.750–3.000 | 30 | AMS 4162, AMS 4163 |
| 7049-T73511 | Extrusion | ST | 0.750–2.999 | 41b | AMS 4157 |
| 3.000–5.000 | 40c | ||||
| 7049-T76511d | Extrusion | ST | 0.750–5.000 | 20 | AMS 4159 |
| 7050-T73511 | Extrusion | ST | 0.750–5.000 | 45 | AMS 4341 |
| 7050-T74511 | Extrusion | ST | 0.750–5.000 | 35 | AMS 4342 |
| 7050-T76511 | Extrusion | ST | 0.750–5.000 | 17 | AMS 4340 |
| 7075-T73-T73510-T73511 | Extrusion | ST | 0.750–1.499 | 45b | AMS-QQ-A-200/11, AMS 4166, AMS 4167, ASTM B 211 |
| 1.500–2.999 | 44b | ||||
| 3.000–4.999 | 42b | ||||
| 3.000–4.999 | 41b,e | ||||
| 7075-T76-T76510-T76511 | Extrusion | ST | 0.750–1.000 | 25 | AMS-QQ-A-200/15, ASTM B 221 |
| 7149-T73511d | Extrusion | ST | 0.750–2.999 | 41c | AMS 4543 |
| 3.000–5.000 | 40c | ||||
| 7150-T77511 | Extrusion | ST | 0.750–2.000 | 25 | AMS 4345 |
| 7175-T73511 | Extrusion | ST | 0.750–2.000 | 44 | AMS 4344 |
| a Most specifications reference ASTM G 47, which requires exposures of 10 days for 2XXX alloys and 20 days for 7XXX alloys in ST test direction. | |||||
| b 75% of specified minimum longitudinal yield strength. | |||||
| c 65% of specified minimum longitudinal yield strength. | |||||
| d Design values are not included in MIL-HDBK-5. | |||||
| e Over 20 square inches cross-sectional area. | |||||
| DO NOT USE STRESS VALUES FOR DESIGN | |||||
| Alloy and Temper | Test Direction | Thickness, inches | Stress, ksi | Referenced Specifications |
|---|---|---|---|---|
| 7049-T73 | ST | 0.750–2.000 | 46b | AMS-QQ-A-367, AMS 4111, ASTM B 247 |
| 2.001–5.000 | 45b | |||
| 7050-T74 | ST | 0.750–6.000 | 35 | AMS 4107 |
| 7050-T7452 | ST | 0.750–4.000 | 35 | AMS 4333 |
| 7075-T73 | ST | 0.750–3.000 | 42b | AMS-A-22771, AMS-QQ-A-367 |
| 3.001–4.000 | 41b | AMS 4241, ASTM B 247 | ||
| 4.001–5.000 | 39b | AMS 4141 | ||
| 5.001–6.000 | 38b | |||
| 7075-T7352 | ST | 0.750–4.000 | 42b | AMS-A-22771, AMS-QQ-A-367, AMS 4147, ASTM B 247 |
| 3.001–4.000 | 39b | |||
| 7075-T7354c | ST | 0.750–3.000 | 42 | Company Specification |
| 7075-T74c | ST | 0.750–3.000 | 35 | AMS 4131 |
| 3.001–4.000 | 31d | |||
| 4.001–5.000 | 30d | |||
| 5.001–6.000 | 29d | |||
| 7149-T73 | ST | 0.750–2.000 | 46b | AMS 4320 |
| 2.001–5.000 | 45b | |||
| 7175-T74 | ST | 0.750–3.000 | 35 | AMS 4149, ASTM B 247 |
| 3.001–4.000 | 31d | AMS 4149 | ||
| 4.001–5.000 | 30d | |||
| 5.001–6.000 | 29d | |||
| 7175-T7452c | ST | 0.750–3.000 | 35 | AMS 4179 |
| a Most specifications reference ASTM G 47, which requires 20 days of exposure for 7XXX alloys in ST test direction. | ||||
| b 75% of specified minimum longitudinal yield strength. | ||||
| c Design values are not included in MIL-HDBK-5. | ||||
| d 50% of specified minimum longitudinal yield strength. | ||||
| Transcription note: This table reproduces MIL-HDBK-5 exactly as published; no values have been altered or corrected. The thickness bands shown for 7075-T7352 (0.750–4.000 followed by 3.001–4.000) overlap in the source document and are reproduced as printed. | ||||
| DO NOT USE STRESS VALUES FOR DESIGN | ||||
| Alloy and Temper | Test Direction | Thickness, inches | Stress, ksi | Referenced Specifications |
|---|---|---|---|---|
| 7049-T73 | ST | 2.001–3.000 | 45b | AMS-QQ-A-367, AMS 4111, ASTM B 247 |
| 3.001–4.000 | 44b | |||
| 4.001–5.000 | 42b | |||
| 7049-T7352c | ST | 0.750–3.000 | 44b | AMS 4247 |
| 3.001–4.000 | 43b | |||
| 4.001–5.000 | 40b | |||
| 7050-T7452 | ST | 0.750–8.000 | 35 | AMS 4108 |
| 7075-T73 | ST | 0.750–3.000 | 42b | AMS-A-22771, AMS-QQ-A-367, |
| 3.001–4.000 | 41b | ASTM B 247 | ||
| 4.001–4.000 | 39b | |||
| 5.001–6.000 | 38b | |||
| 7075-T7352 | ST | 0.750–3.000 | 39d | |
| 3.001–4.000 | 37d | AMS 4147 | ||
| 4.001–5.000 | 36d | |||
| 5.001–6.000 | 34d | |||
| 7075-T74e | ST | 0.750–3.000 | 35 | |
| 3.001–4.000 | 30e | AMS 4131 | ||
| 4.001–5.000 | 28e | |||
| 5.001–6.000 | 27e | |||
| 7075-T7452c | ST | 0.750–2.000 | 35 | |
| 2.001–3.000 | 29f | AMS 4323 | ||
| 3.001–4.000 | 28f | |||
| 4.001–5.000 | 26f | |||
| 5.001–6.000 | 24f | |||
| 7149-T73 | ST | 2.000–3.000 | 44d | |
| 3.001–4.000 | 43d | AMS 4320 | ||
| 4.001–5.000 | 42d | |||
| 7175-T74 | ST | 0.750–3.000 | 35 | |
| 3.001–4.000 | 29f | AMS 4149 | ||
| 4.001–5.000 | 28f | |||
| 4.001–6.000 | 26f | |||
| 7175-T7452 | ST | 0.750–3.000 | 35 | |
| 3.001–4.000 | 27f | AMS 4179 | ||
| 4.001–5.000 | 26f | |||
| 5.001–6.000 | 24f | |||
| a Most specifications reference ASTM G 47, which requires 20 days of exposure for 7XXX alloys in ST test direction. | ||||
| b 75% of specified minimum longitudinal yield strength. | ||||
| c Design values are not included in MIL-HDBK-5. | ||||
| d 75% of specified minimum long transverse yield strength. | ||||
| e 50% of specified minimum longitudinal yield strength. | ||||
| f 50% of specified minimum long transverse yield strength. | ||||
| Transcription note: This table reproduces MIL-HDBK-5 exactly as published; no values have been altered or corrected. Three entries appear anomalous in the source and are reproduced as printed: the 7075-T73 band listed as 4.001–4.000; the 7175-T74 band listed as 4.001–6.000, which repeats the start of the preceding band; and the superscript e attached to the alloy designation 7075-T74, where footnote e defines a yield-strength percentage rather than a product qualifier. | ||||
| DO NOT USE STRESS VALUES FOR DESIGN | ||||
3.1.2.3.2 Resistance to Exfoliation [Reference 3.1.2.3.2] — The high-strength wrought aluminum alloys in certain tempers are susceptible to exfoliation corrosion, dependent upon product and section size. Generally those alloys and tempers that have the lowest resistance to stress-corrosion cracking also have the lowest resistance to exfoliation. The tempers that provide improved resistance to stress-corrosion cracking also provide improved resistance or immunity to exfoliation. For example, the T76 temper of 7075, 7049, 7050, and 7475 provides a very high resistance to exfoliation, i.e., decidedly superior to the T6 temper, and almost the immunity provided by the T73 temper of 7075 alloy (see Reference 3.1.2.3.2).
In order to avoid stress-corrosion cracking (see Section 3.1.2.3), practices, such as the use of press or shrink fits; taper pins; clevis joints in which tightening of the bolt imposes a bending load on female lugs; and straightening or assembly operations; which result in sustained surface tensile stresses (especially when acting in the short-transverse grain orientation), should be avoided in these high-strength alloys: 2014-T451, T4, T6, T651, T652; 2024-T3, T351, T4; 7075-T6, T651, T652; 7150-T6151, T61511; and 7475-T6, T651.
Where straightening or forming is necessary, it should be performed when the material is in the freshly quenched condition or at an elevated temperature to minimize the residual stress induced. Where elevated temperature forming is performed on 2014-T4 T451, or 2024-T3 T351, a subsequent precipitation heat treatment to produce the T6 or T651, T81 or T851 temper is recommended.
It is good engineering practice to control sustained short-transverse tensile stress at the surface of structural parts at the lowest practicable level. Thus, careful attention should be given in all stages of manufacturing, starting with design of the part configuration, to choose practices in the heat treatment, fabrication, and assembly to avoid unfavorable combinations of end grain microstructure and sustained tensile stress. The greatest danger arises when residual, assembly, and service stress combine to produce high sustained tensile stress at the metal surface. Sources of residual and assembly stress have been the most contributory to stress-corrosion-cracking problems because their presence and magnitude were not recognized. In most cases, the design stresses (developed by functional loads) are not continuous and would not be involved in the summation of sustained tensile stress. It is imperative that, for materials with low resistance to stress-corrosion cracking in the short-transverse grain orientation, every effort be taken to keep the level of sustained tensile stress close to zero.
Cold working such as stretch forming of aluminum alloy prior to solution heat treatment may result in recrystallization or grain growth during heat treatment. The resulting strength, particularly yield strength, may be significantly below the specified minimum values. For critical applications, the strength should be determined on the part after forming and heat treating including straightening operations. To minimize recrystallization during heat treatment, it is recommended that forming be done after solution heat treatment in the as-quenched condition whenever possible, but this may result in compressive yield strength in the direction of stretching being lower than MIL-HDBK-5 design allowables for user heat treat tempers.
The dimensional changes that occur in aluminum alloy during thermal treatment generally are negligible, but in a few instances these changes may have to be considered in manufacturing. Because of many variables involved, there are no tabulated values for these dimensional changes. In the artificial aging of alloy 2219 from the T42, T351, and T37 tempers to the T62, T851, and T87 tempers, respectively, a net dimensional growth of 0.00010 to 0.0015 in./in. may be anticipated. Additional growth of as much as 0.0010 in./in. may occur during subsequent service of a year or more at 300°F or equivalent shorter exposures at higher temperatures. The dimensional changes that occur during the artificial aging of other wrought heat-treatable alloys are less than one-half that for alloy 2219 under the same conditions.
The ease with which aluminum alloys may be welded is dependent principally upon composition, but the ease is also influenced by the temper of the alloy, the welding process, and the filler metal used. Also, the weldability of wrought and cast alloys is generally considered separately.
Several weldability rating systems are established and may be found in publications by the Aluminum Association, American Welding Society, and the American Society for Metals. Handbooks from these groups can be consulted for more detailed information. Specification AA-R-566 also contains useful information. This document follows most of these references in adopting a four level rating system. An “A” level, or readily weldable, means that the alloy (and temper) is routinely welded by the indicated process using commercial procedures. A “B” level means that welding is accomplished for many applications, but special techniques are required, and the application may require preliminary trials to develop procedures and tests to demonstrate weld performance. A “C” level refers to limited weldability because crack sensitivity, loss of corrosion resistance, and/or loss of mechanical properties may occur. A “D” level indicates that the alloy is not commercially weldable.
The weldability of aluminum alloys is rated by alloy, temper, and welding process (arc or resistance). Tables 3.1.3.4(a) and (b) list the ratings in the alloy section number order in which they appear in Chapter 3.
When heat-treated or work-hardened materials of most systems are welded, a loss of mechanical properties generally occurs. The extent of the loss (if not reheat treated) over the table strength allowables will have to be established for each specific situation.
| MIL-HDBK-5 Section No. | Alloy | Tempers | Weldabilitya,b | |
|---|---|---|---|---|
| Inert Gas Metal or Tungsten Arc | Resistance Spotc | |||
| 3.2.1 | 2014 | O | C | D |
| T6, T62, T651, T652, T6510, T6511 | B | B | ||
| 3.2.2 | 2017 | T4, T42, T451 | C | B |
| 3.2.3 | 2024 | O | D | D |
| T3, T351, T361, T4, T42 | C | B | ||
| T6, T62, T81, T851, T861 | C | B | ||
| T8510, T8511, T3510, T3511 | C | B | ||
| 3.2.4 | 2025 | T6 | C | B |
| 3.2.5 | 2090 | T83 | B | B |
| 3.2.6 | 2124 | T851 | C | B |
| 3.2.7 | 2219 | O | A | B-D |
| T62, T81, T851, T87, T8510, T8511 | A | A | ||
| 3.2.8 | 2618 | T61 | C | B |
| 3.2.9 | 2519 | T87 | A | … |
| 3.5.1 | 5052 | O | A | A |
| H32, H34, H36, H38 | A | A | ||
| 3.5.2 | 5083 | O | A | A |
| H321, H323, H343, H111, H112 | A | B | ||
| 3.5.3 | 5086 | O | A | A |
| H32, H34, H36, H38, H111, H112 | A | B | ||
| 3.5.4 | 5454 | O | A | A |
| H32, H34, H111, H112 | A | B | ||
| 3.5.5 | 5456 | O | A | A |
| H111, H321, H112 | A | B | ||
| 3.6.1 | 6013 | T6 | A | A |
| 3.6.2 | 6061 | O | A | A |
| T4, T42, T451, T4510, T4511, T6 | A | A | ||
| T62, T651, T652, T6510, T6511 | A | A | ||
| 3.6.3 | 6151 | T6 | A | A |
| 3.7.1 | 7010 | All | C | B |
| 3.7.2 | 7040 | All | C | B |
| 3.7.3 | 7049 7149 | All | C | B |
| 3.7.4 3.7.5 | 7050 7055 | All | C | B |
| 3.7.6 | 7075 | All | C | B |
| 3.7.7 | 7150 | All | C | B |
| 3.7.8 | 7175 | All | C | B |
| 3.7.9 3.7.10 | 7249 7475 | All | C | B |
| a Ratings A through D are relative ratings defined as follows: A — Generally weldable by all commercial procedures and methods. B — Weldable with special techniques or for specific applications which justify preliminary trials or testing to develop welding procedures and weld performance. C — Limited weldability because of crack sensitivity or loss in resistance to corrosion and mechanical properties. D — No commonly used welding methods have been developed. | ||||
| b When using filler wire, the wire should contain less than 0.0008 percent beryllium to avoid toxic fumes. | ||||
| c See AMS-W-6858 for permissible combinations. | ||||
| MIL-HDBK-5 Section No. | Alloy | Weldabilityb,c | |
|---|---|---|---|
| Inert Gas Metal or Tungsten Arc | Resistance Spot | ||
| 3.8.1 | A201.0 | C | C |
| 3.9.1 | 354.0 | B | B |
| 3.9.2 | 355.0 | B | B |
| 3.9.3 | C355.0 | B | B |
| 3.9.4 | 356.0 | A | A |
| 3.9.5 | A356.0 | A | A |
| 3.9.6 | A357.0 | A | B |
| 3.9.7 | D357.0 | A | B |
| 3.9.8 | 359.0 | A | B |
| a Weldability related to joining a casting to another part of same composition. The weldability ratings are not applicable to minor weld repairs. Such repairs will be governed by the contractors procedure for in-process welding of castings, after approval by the procuring agency. | |||
| b Ratings A through D are relative ratings defined as follows: A — Generally weldable by all commercial procedures and methods. B — Weldable with special techniques or for specific applications which justify preliminary trials or testing to develop welding procedure and weld performance. C — Limited weldability because of crack sensitivity or loss in resistance to corrosion and mechanical properties. D — No commonly used welding methods have been developed. | |||
| c When using filler wire, the wire should contain less than 0.0008 percent beryllium to avoid toxic fumes. | |||